HEAVY-PLATE BENDING & FORMING
Five bending and rolling machines support drawing-defined cylindrical and curved components, from compact sections to large-diameter heavy-wall workpieces.
Published ranges describe individual machine capabilities. Maximum diameter, thickness and length are not automatically available in one combined workpiece; final feasibility is confirmed from the drawing, material and forming sequence.
Five Machines. One Drawing-Based Review.
Each machine is selected against geometry, plate thickness, workpiece length, material behaviour and downstream welding or machining requirements.
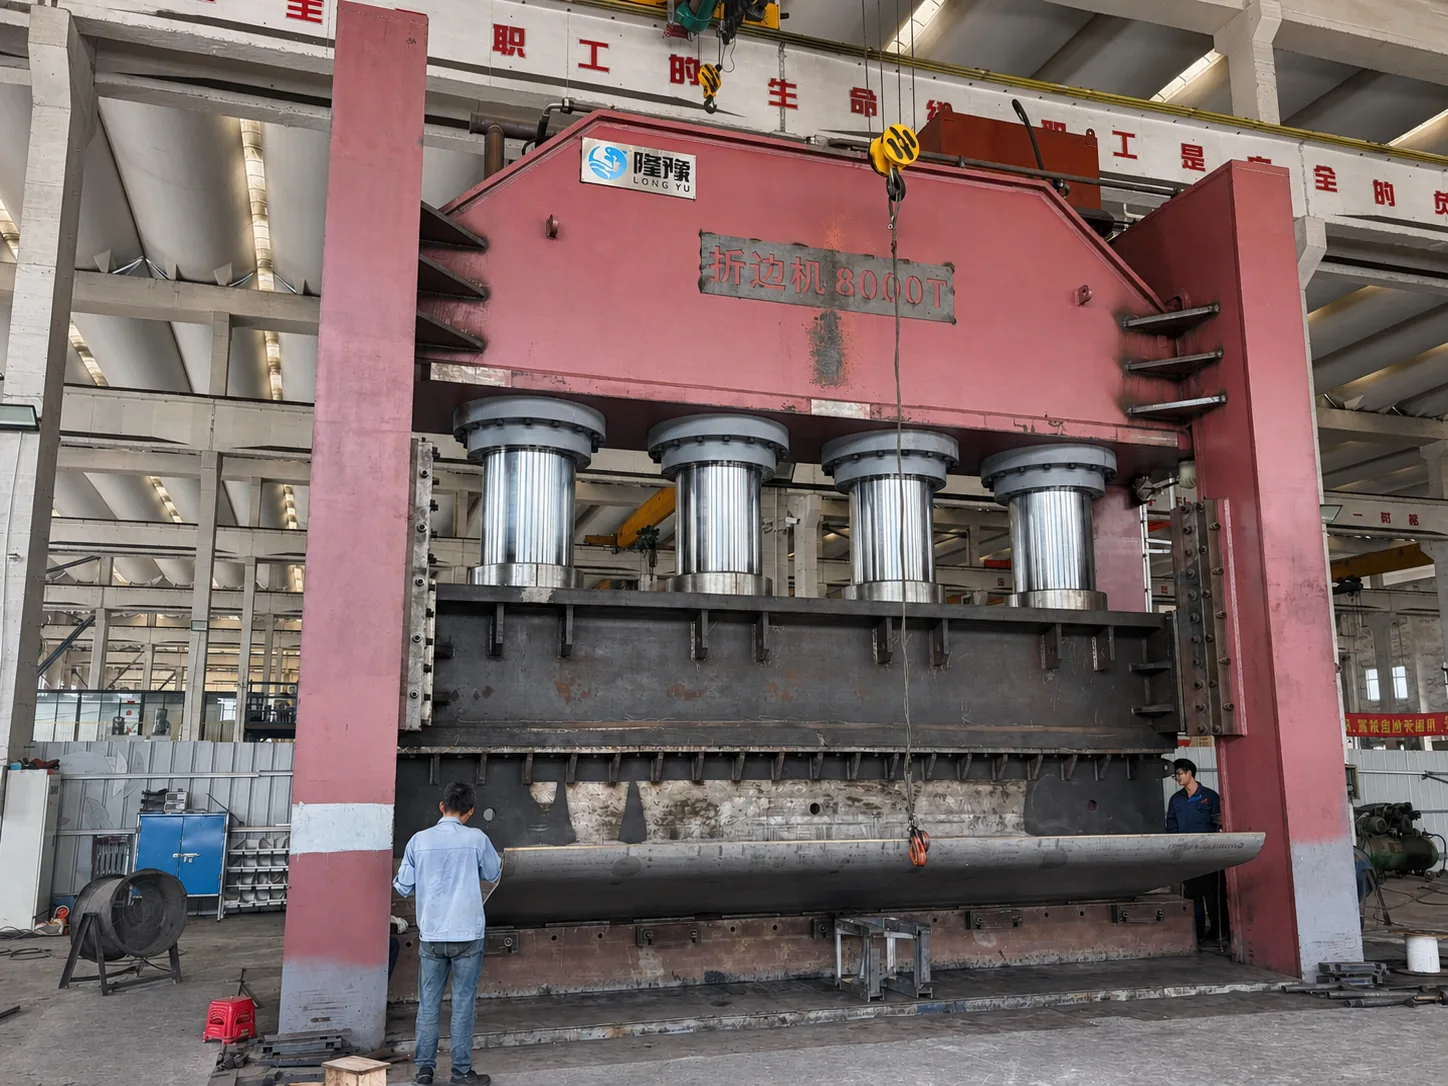
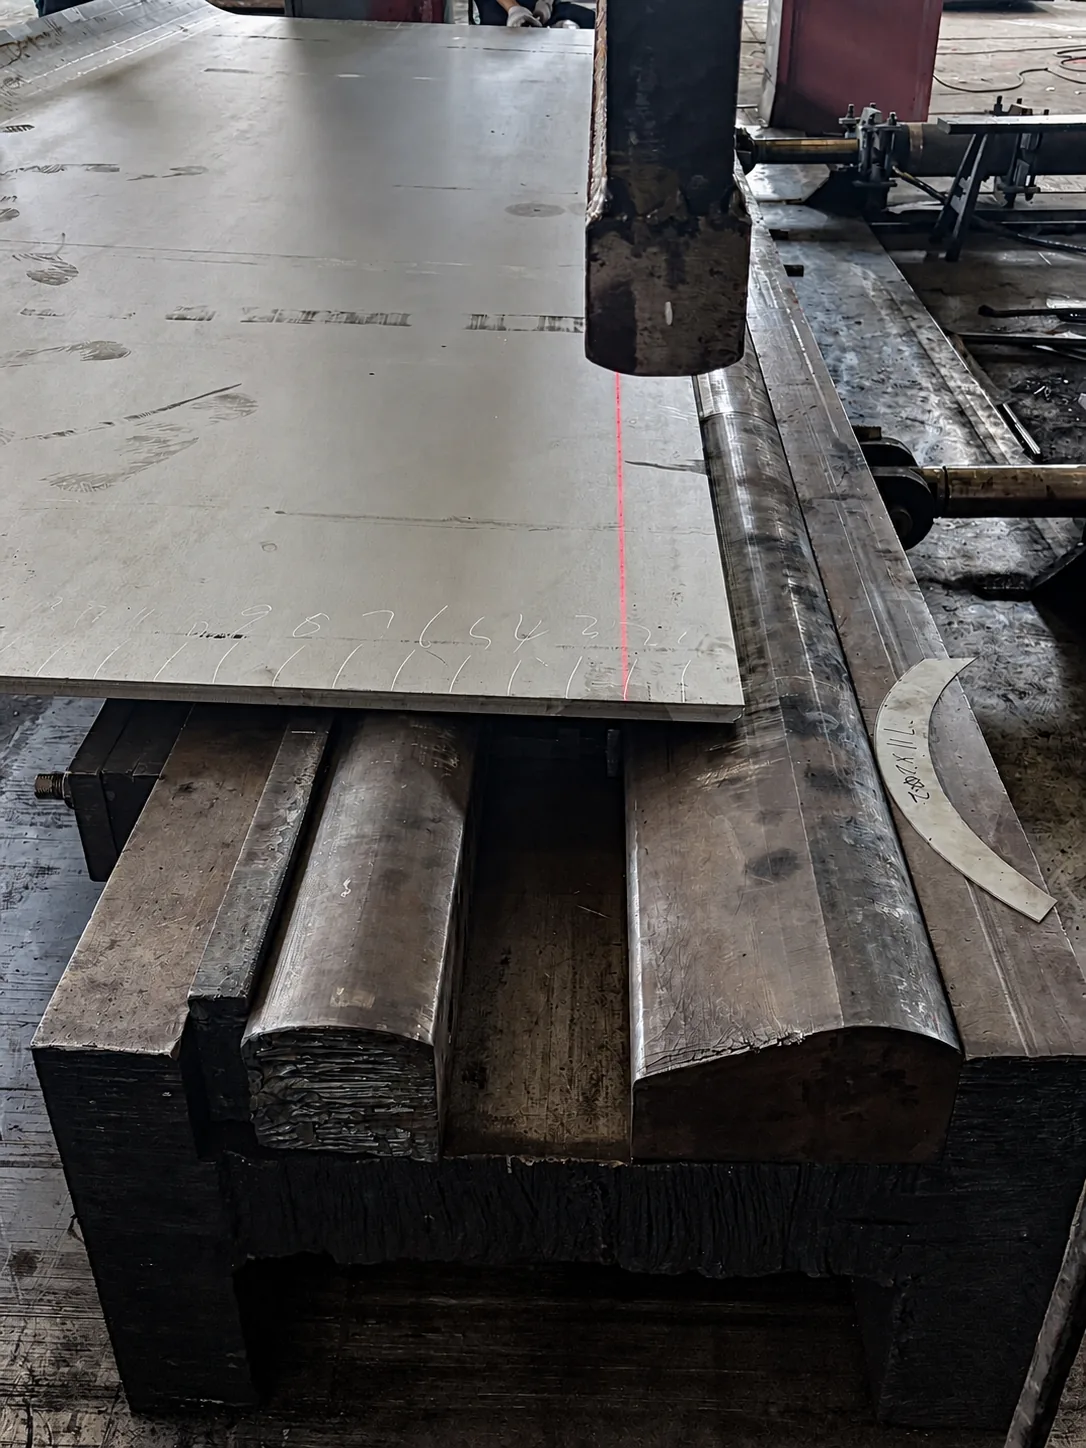
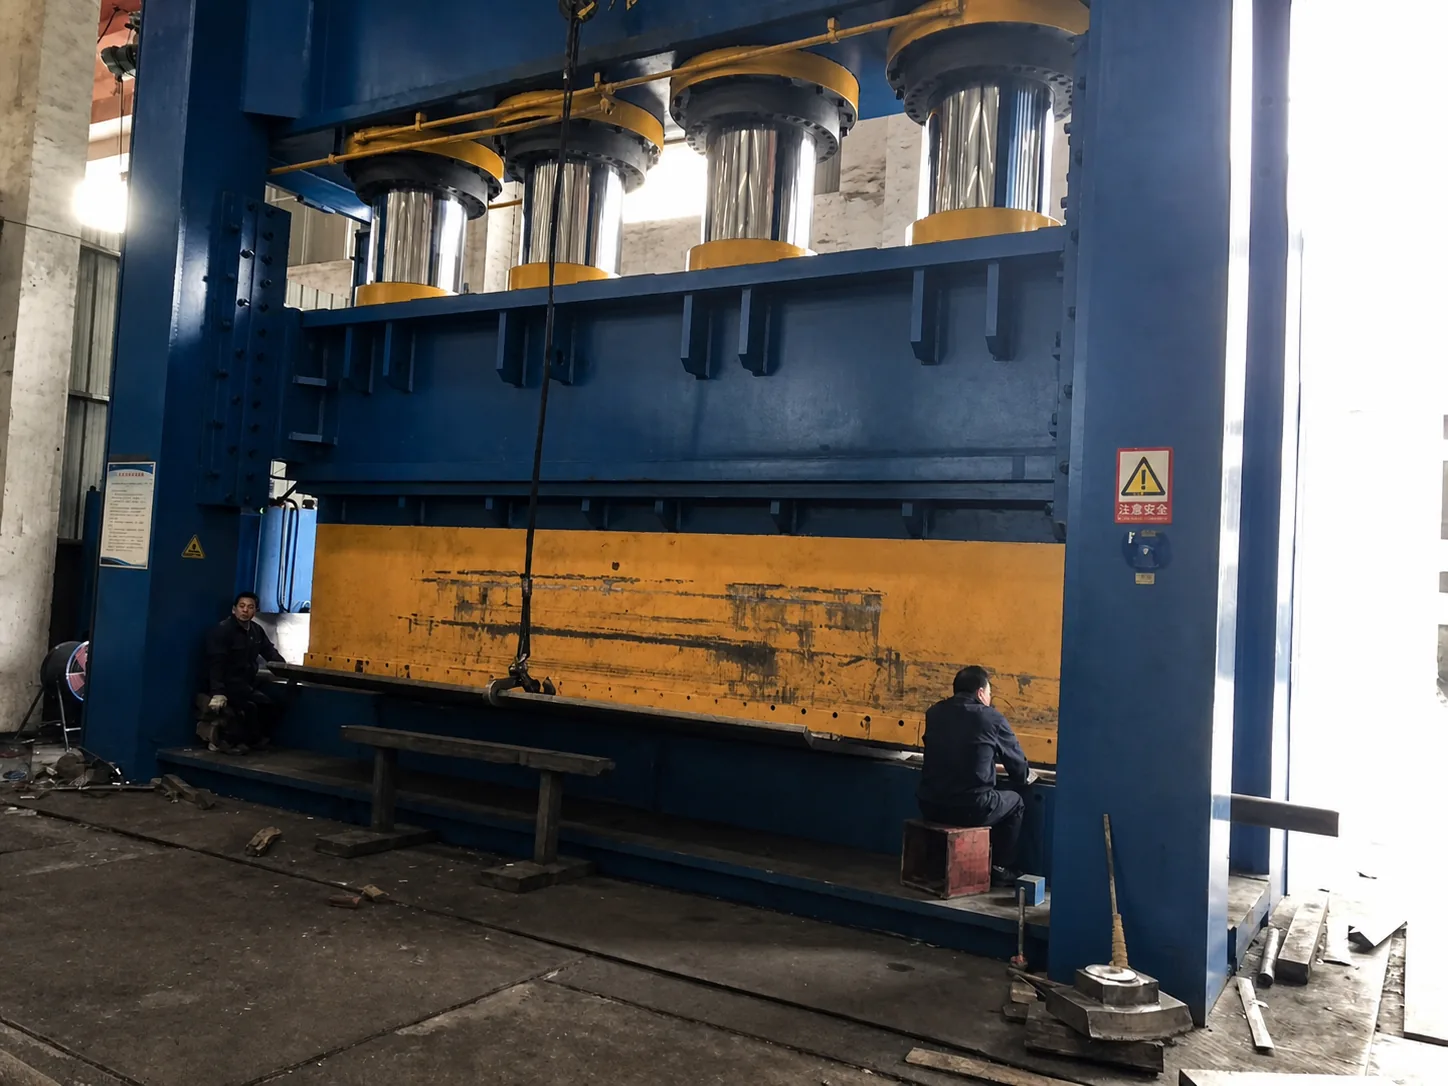
8000-Ton Hydraulic Bending Press
Built for long, large-diameter and heavy-wall forming work. The forming sequence is reviewed from the customer drawing to coordinate curvature, end condition and later welding preparation.
Best suited to drawing-defined large shells, heavy-wall pipe sections and long formed components. Material and geometry remain subject to technical review.
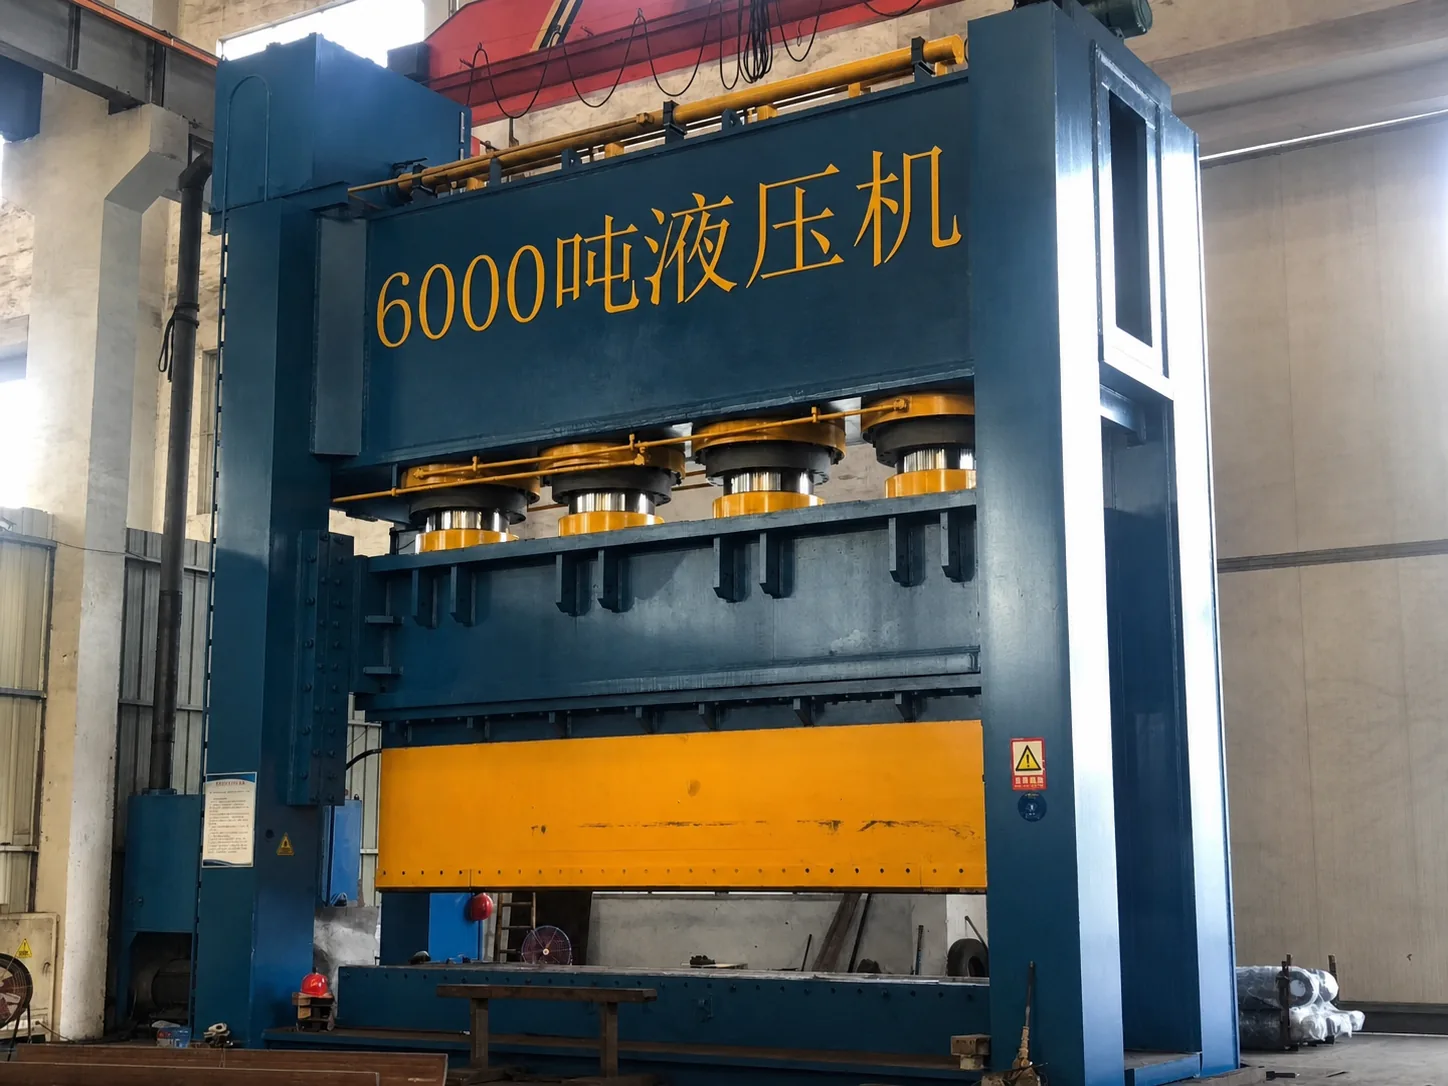
6000-Ton Hydraulic Press
A second heavy-forming route for thick plate and large cylindrical sections. Equipment selection considers the required diameter together with thickness, length, material response and forming sequence.
Used where heavy plate, controlled curvature and a shorter maximum workpiece length make this press the more suitable forming route.
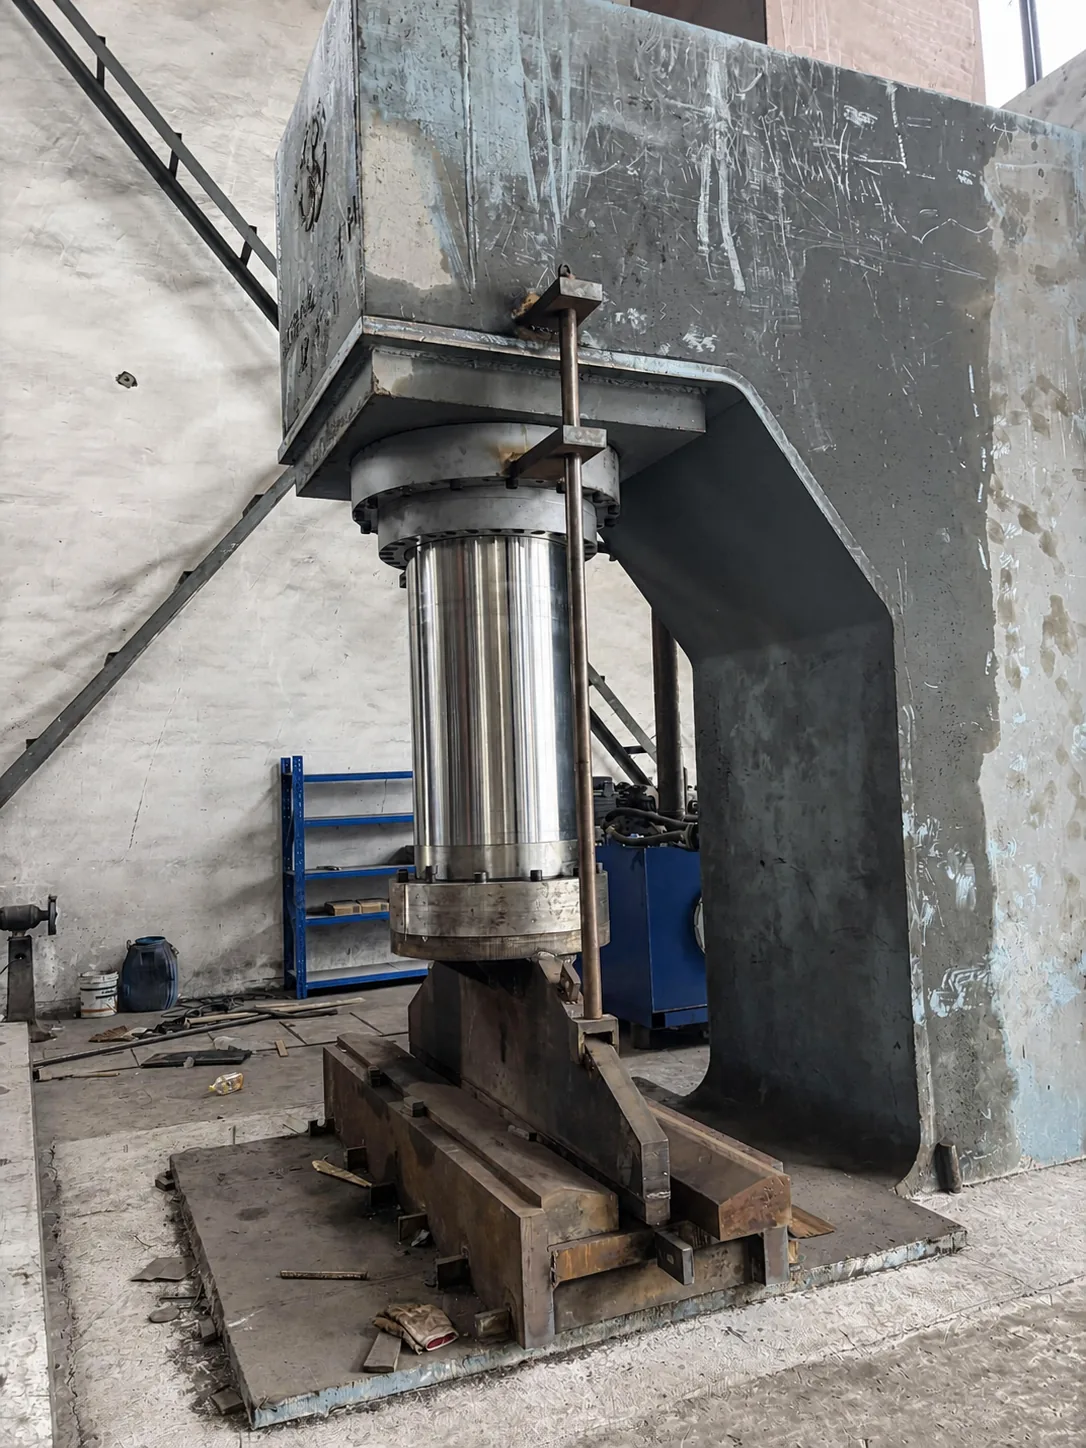
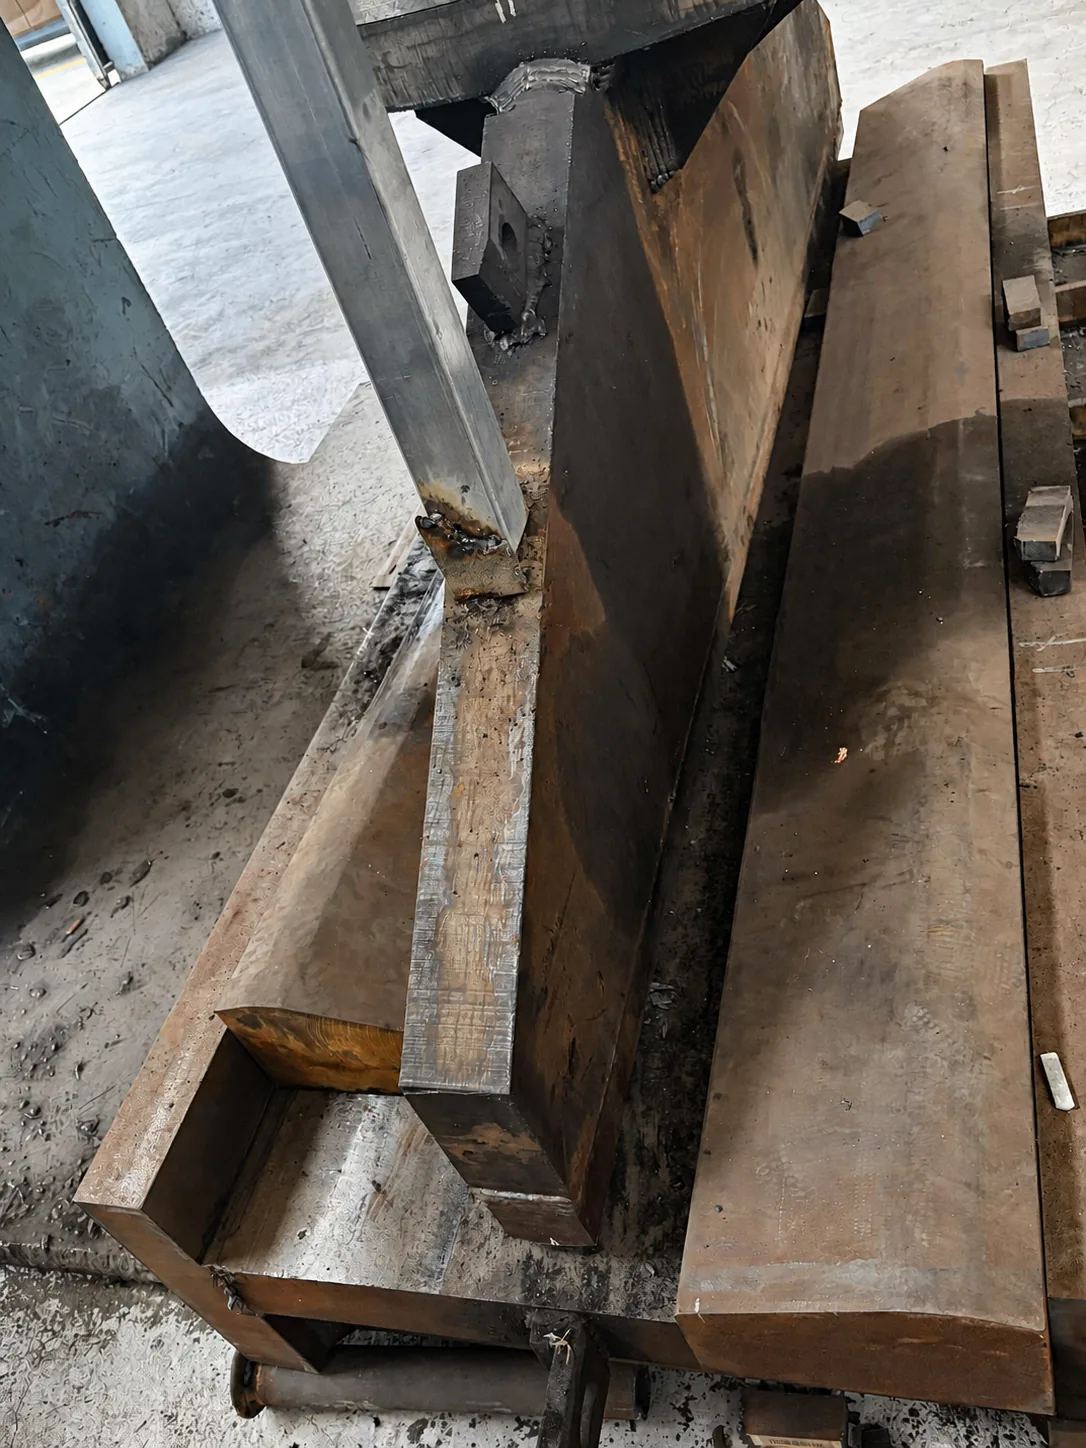
1000-Ton Jaw-Type Bending Press
Supports shorter and smaller-diameter components that require a more compact forming setup. Tooling and forming steps are matched to the section geometry and required end condition.
A practical option for compact formed sections, tighter production setups and short drawing-defined workpieces.
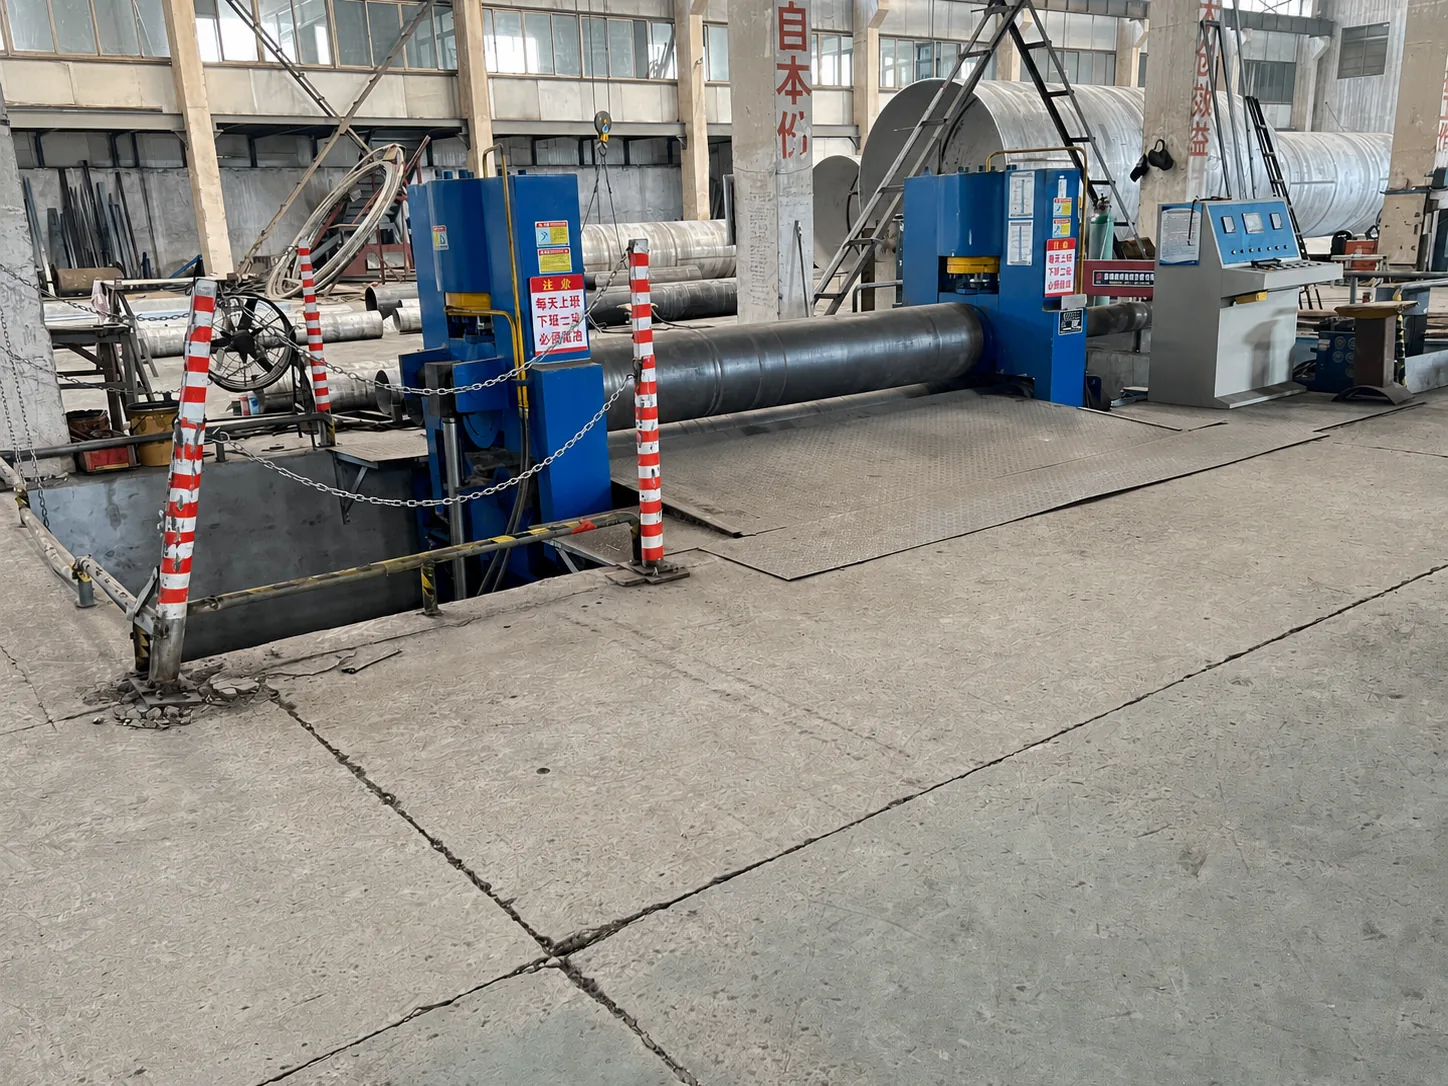
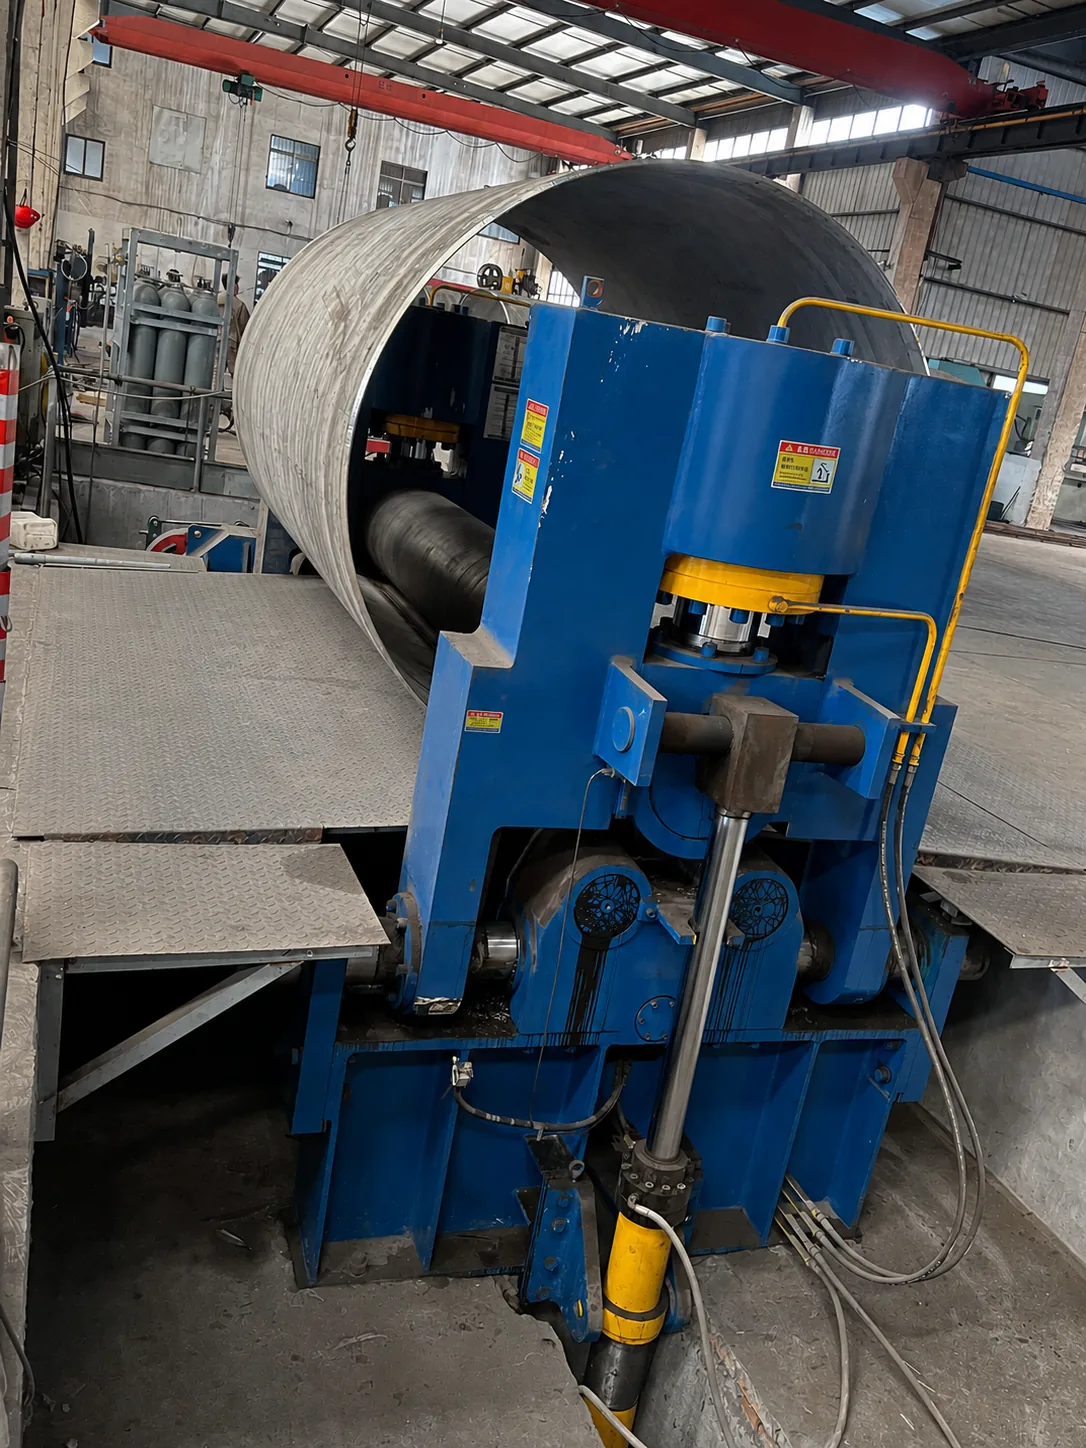
Plate Rolling Machine 01
Progressive plate rolling supports large cylindrical sections and controlled curvature before seam preparation and subsequent fabrication.
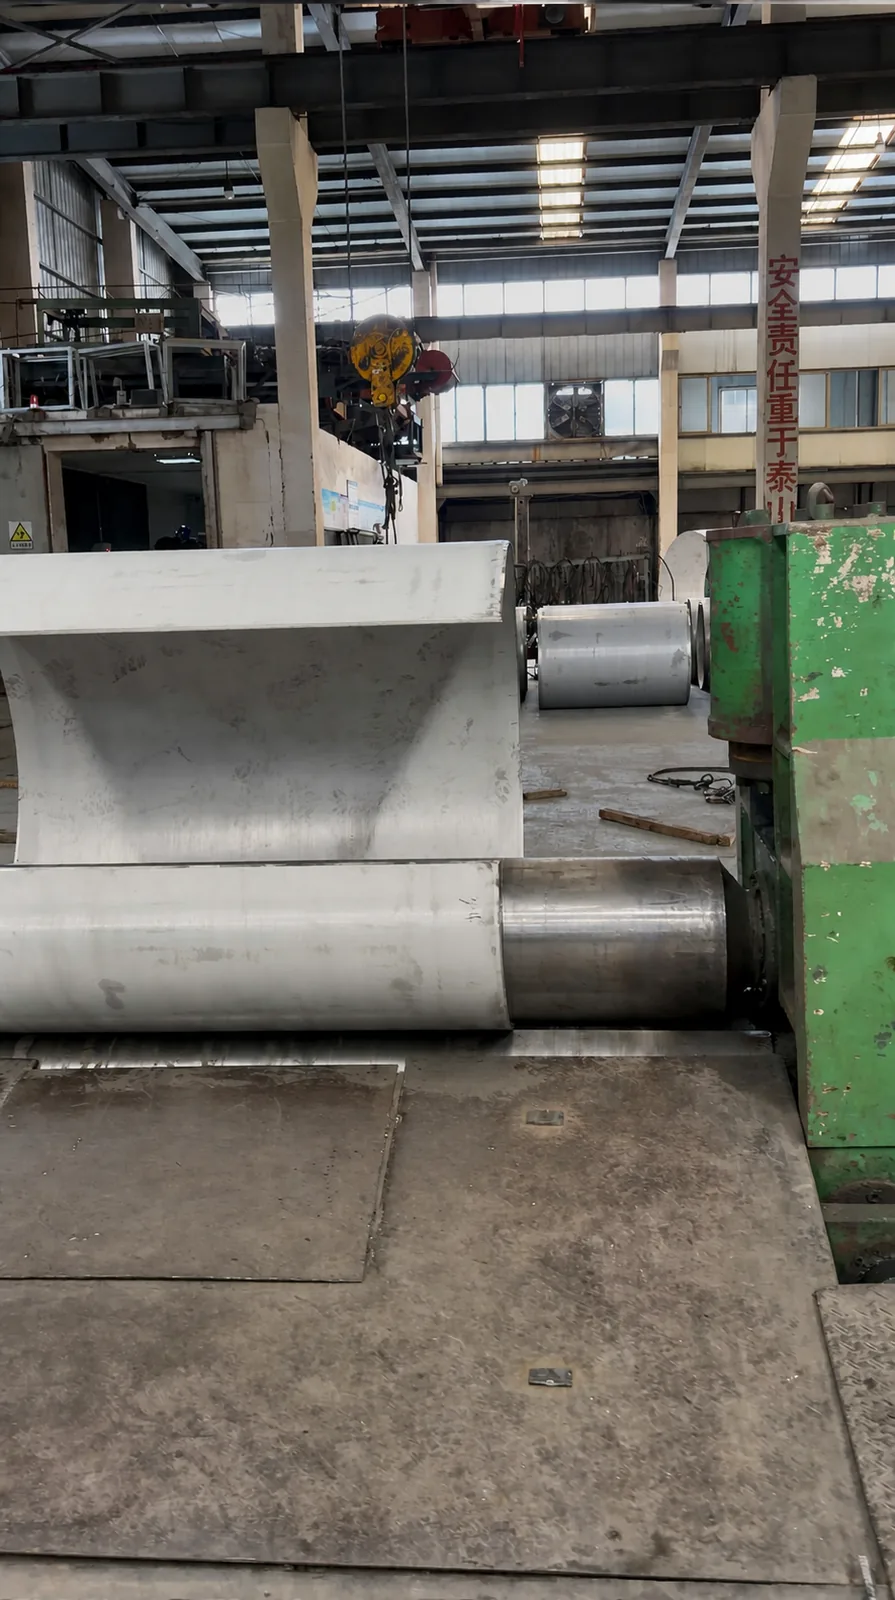
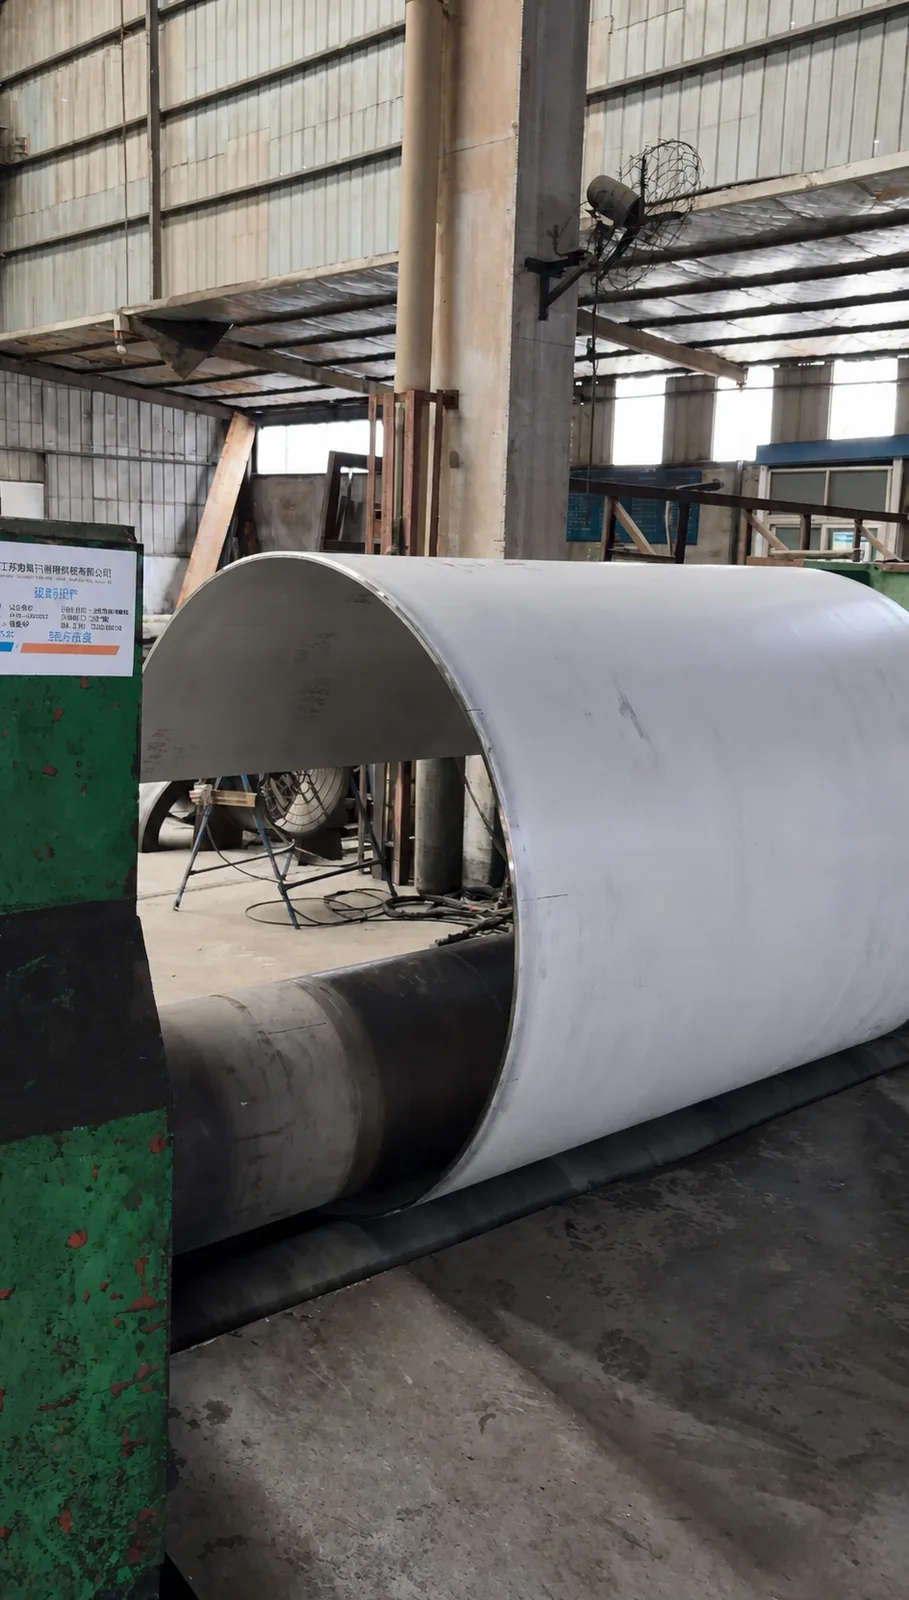
Plate Rolling Machine 02
A parallel rolling route that adds scheduling flexibility for large-diameter shells, pipe sections and custom curved components.
The Right Machine Starts with the Drawing
Diameter alone does not determine the forming method. Plate thickness, material behaviour, workpiece length, tolerances, end preparation and downstream welding requirements are reviewed together.
For non-standard components, the forming route is established around the approved drawing rather than a fixed catalogue size. This keeps equipment selection, fabrication allowances and inspection points aligned before production begins.
Forming Capability Supported by Inspection
Inspection requirements are coordinated with the product, order and agreed acceptance criteria.
Material & Drawing Review
Material grade, dimensions, tolerances and forming notes are reviewed before machine selection.
Diameter & Circumference
Formed geometry is checked against drawing-defined diameter and circumference requirements.
Wall & Geometry Verification
Wall condition, roundness, straightness and end geometry are checked where applicable.
Inspection Documentation
Manufacturing and inspection records are prepared according to the agreed project scope.
Questions Before Technical Review
Which bending machine will be used for my project?
The machine is selected after reviewing diameter, thickness, length, material behaviour, tolerances, end preparation and the downstream fabrication sequence.
Can the maximum diameter, thickness and length be combined?
Published ranges describe individual machine capabilities. Maximum diameter, thickness and length are not automatically available in one combined workpiece. Final feasibility depends on the drawing, material and forming sequence.
Can NOKX form non-standard dimensions?
Yes. Non-standard work is reviewed from the customer drawing. Geometry, tooling, forming steps, inspection points and manufacturing handover are coordinated for the specific project.
Which materials can be formed?
Project-specified metallic grades can be reviewed. Final feasibility depends on grade, thickness, heat condition, forming behaviour, required radius and the applicable project specification.
How are forming dimensions inspected?
Checks may include diameter, circumference, roundness, straightness, wall condition, end geometry and other drawing-defined characteristics, according to the agreed inspection scope.
What information should I provide for technical review?
Please send the drawing, required diameter, wall thickness, length, material grade, quantity, tolerances, end preparation and any inspection or delivery requirements.
Send Your Drawing for a Forming Review
Provide the required diameter, wall thickness, length, material grade, quantity and dimensional requirements. NOKX will review the suitable equipment and forming route.