OUR PROCESS · WELDING
CONTROLLED WELDING FOR INDUSTRIAL COMPONENTS
Plasma arc, TIG, submerged arc and manual welding processes can be combined around material, thickness, joint geometry, applicable standards and inspection requirements.
WELDING METHODS
Five Processes, One Coordinated Route
The process sequence is selected around the joint—not forced into one fixed recipe. Root, fill, cap, internal conditioning and repair can be assigned to different welding methods.
 01
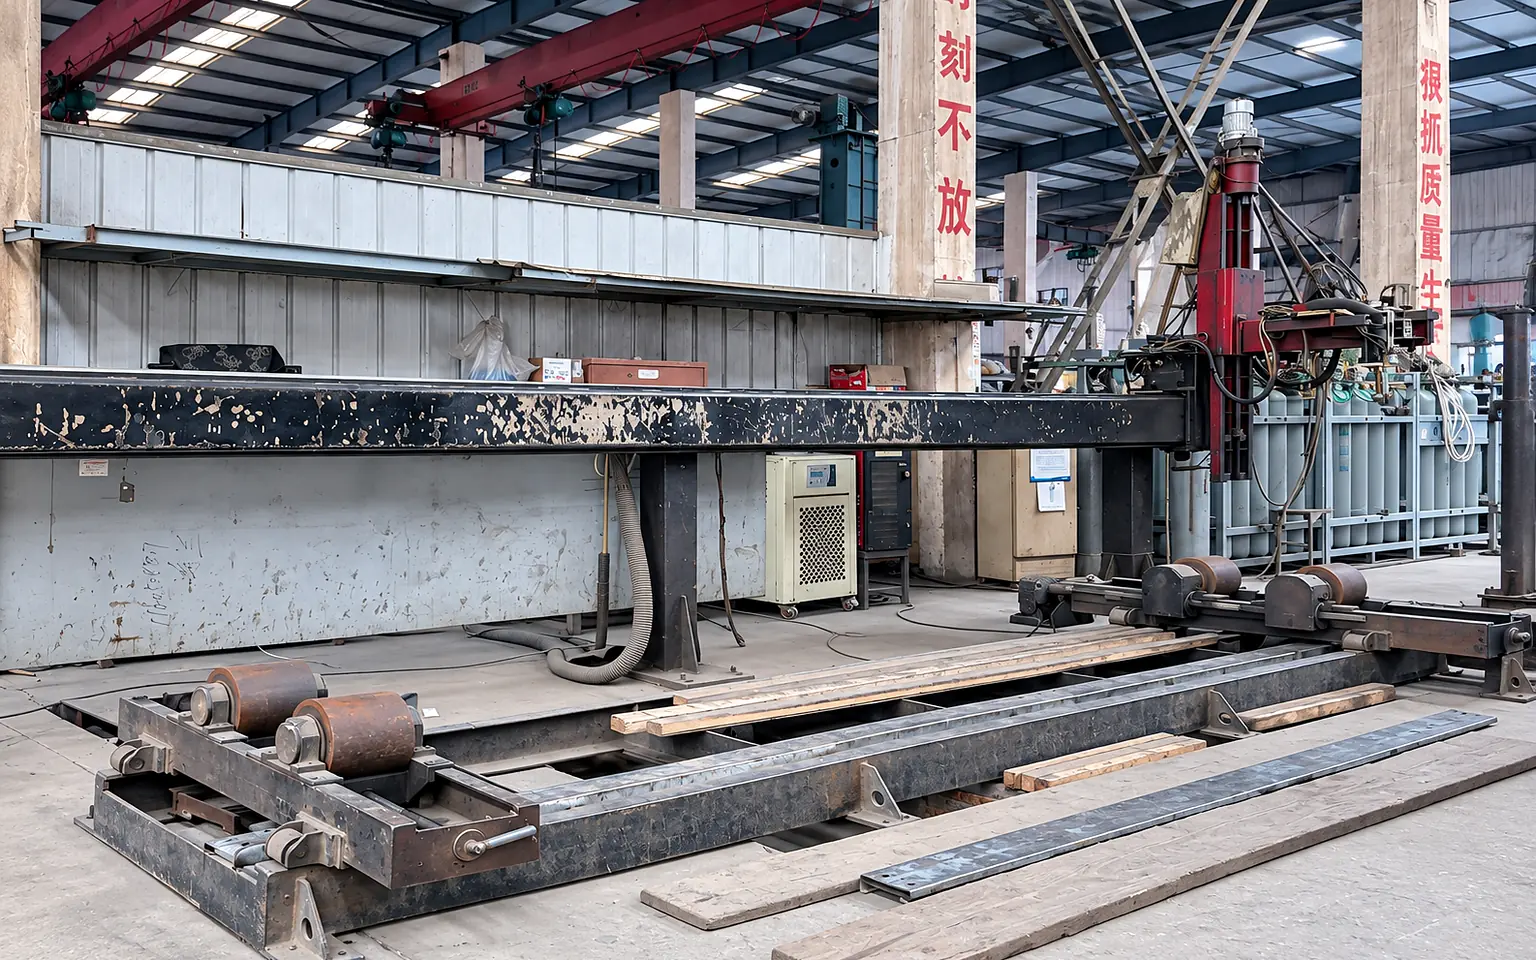
Plasma Arc Welding
PAW · ROOT WELDINGConcentrated arc control supports root penetration and repeatable longitudinal seams. For suitable stainless steel joints at 10 mm and below, a qualified route may achieve single-side welding with back formation.
 02
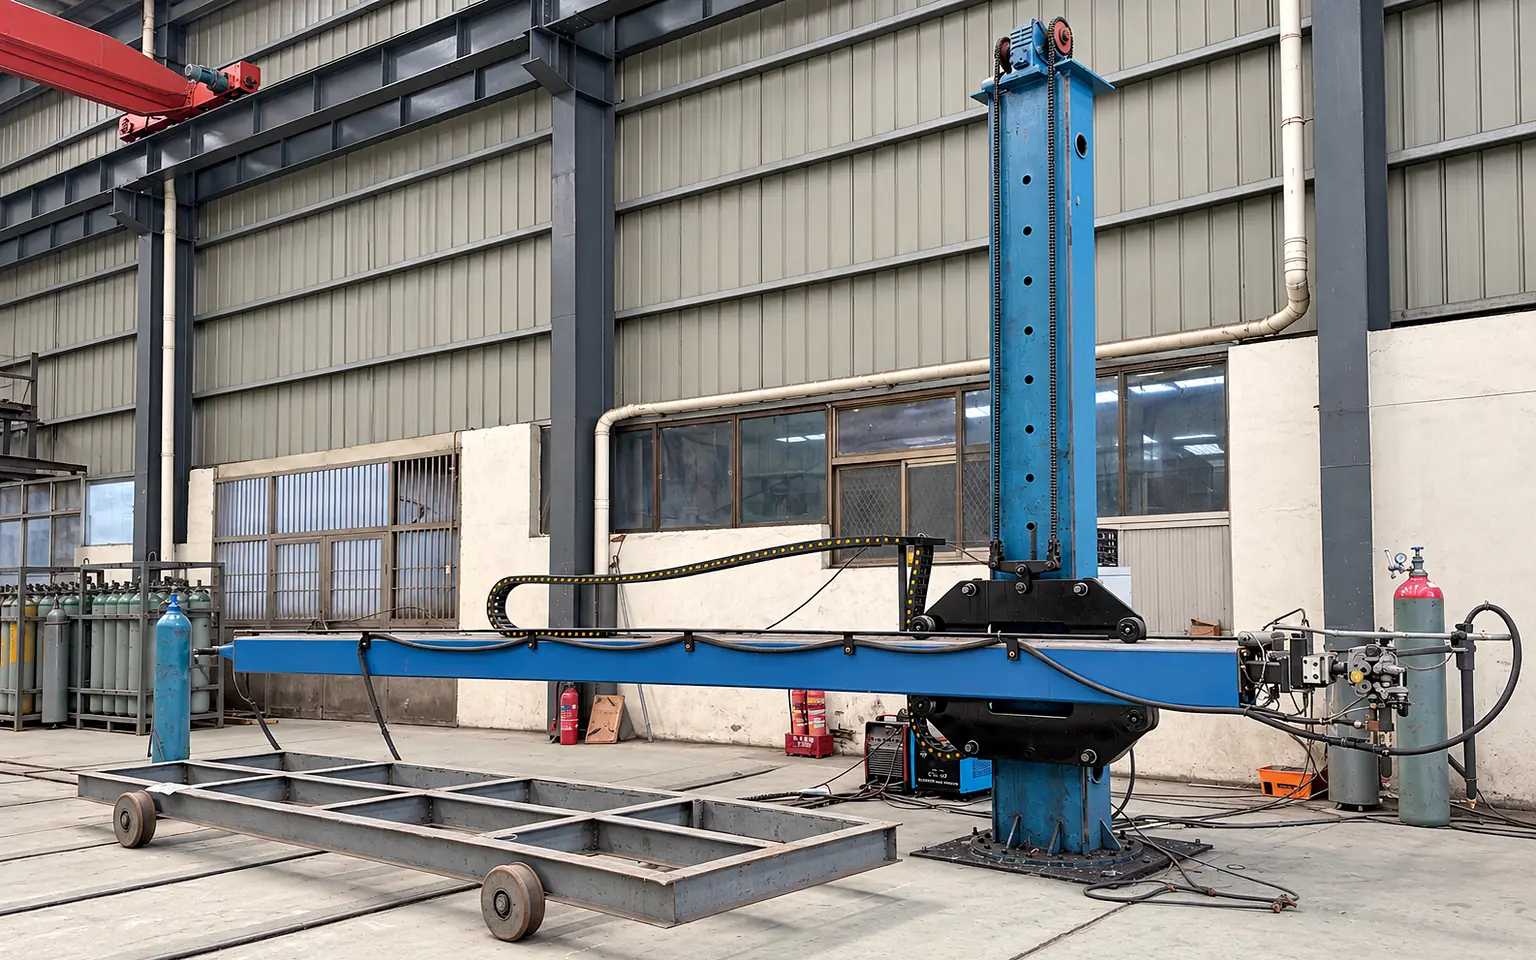
Mechanized TIG Welding
GTAW · FILL, CAP & INTERNAL CONTROLMechanized travel supports consistent bead placement for filling, capping or internal-seam conditioning. Shielding gas, filler metal, pass sequence and interpass control follow the applicable procedure.
 03
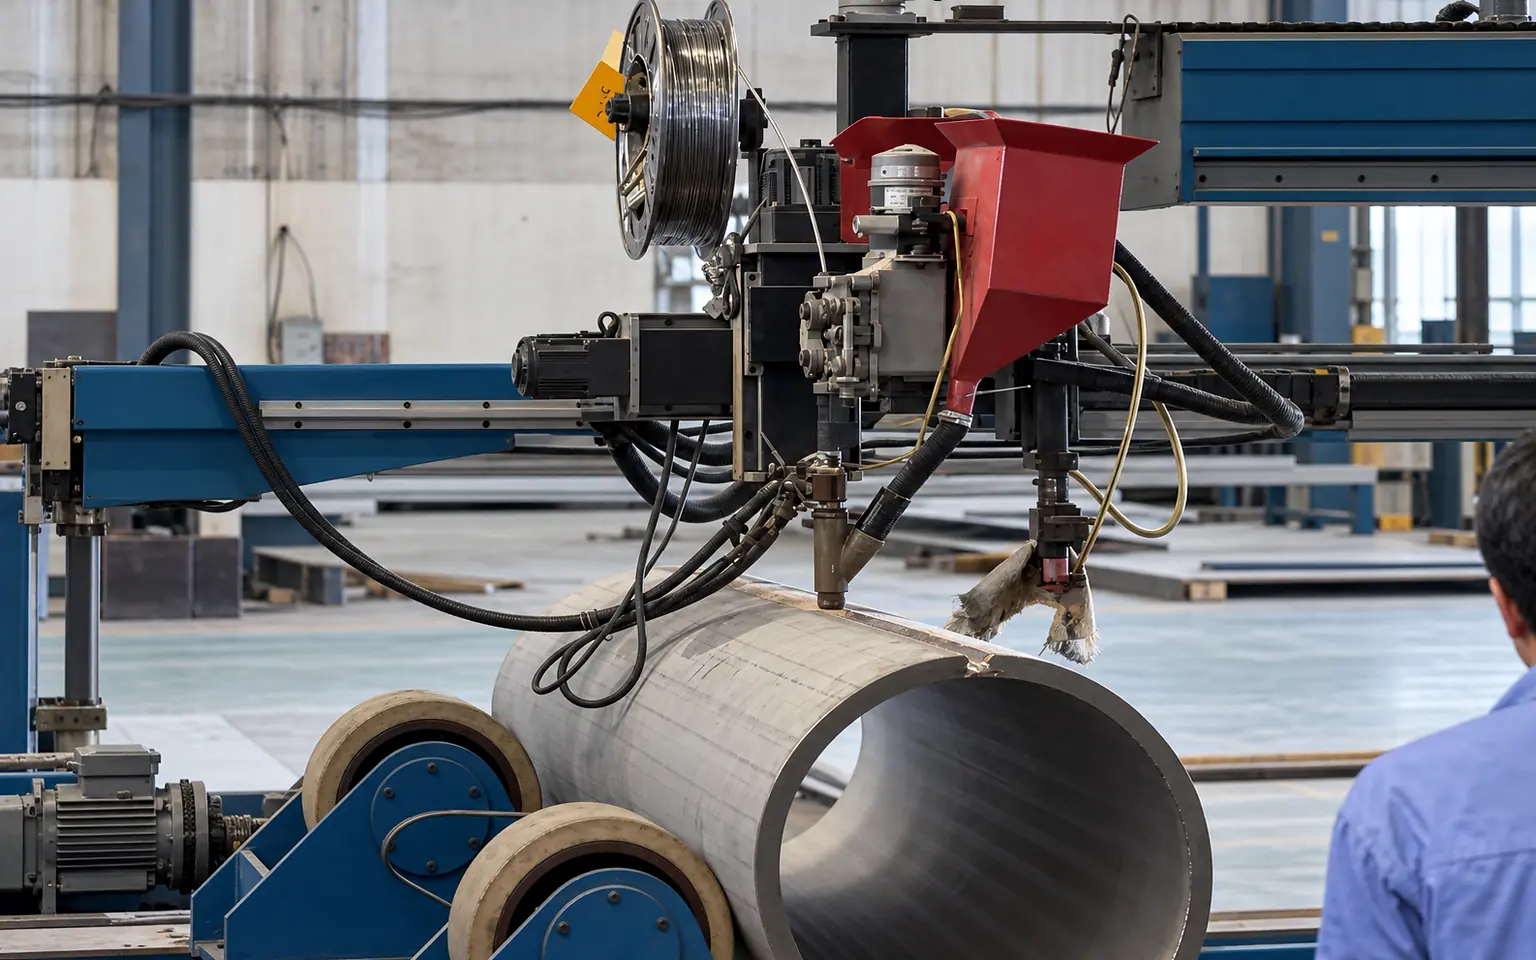
Submerged Arc Welding
SAW · EFFICIENT FILL & CAPWire and flux operate beneath the flux blanket for efficient deposition on suitable long seams. Travel speed, layer cleaning, heat input and joint position are coordinated through the procedure.
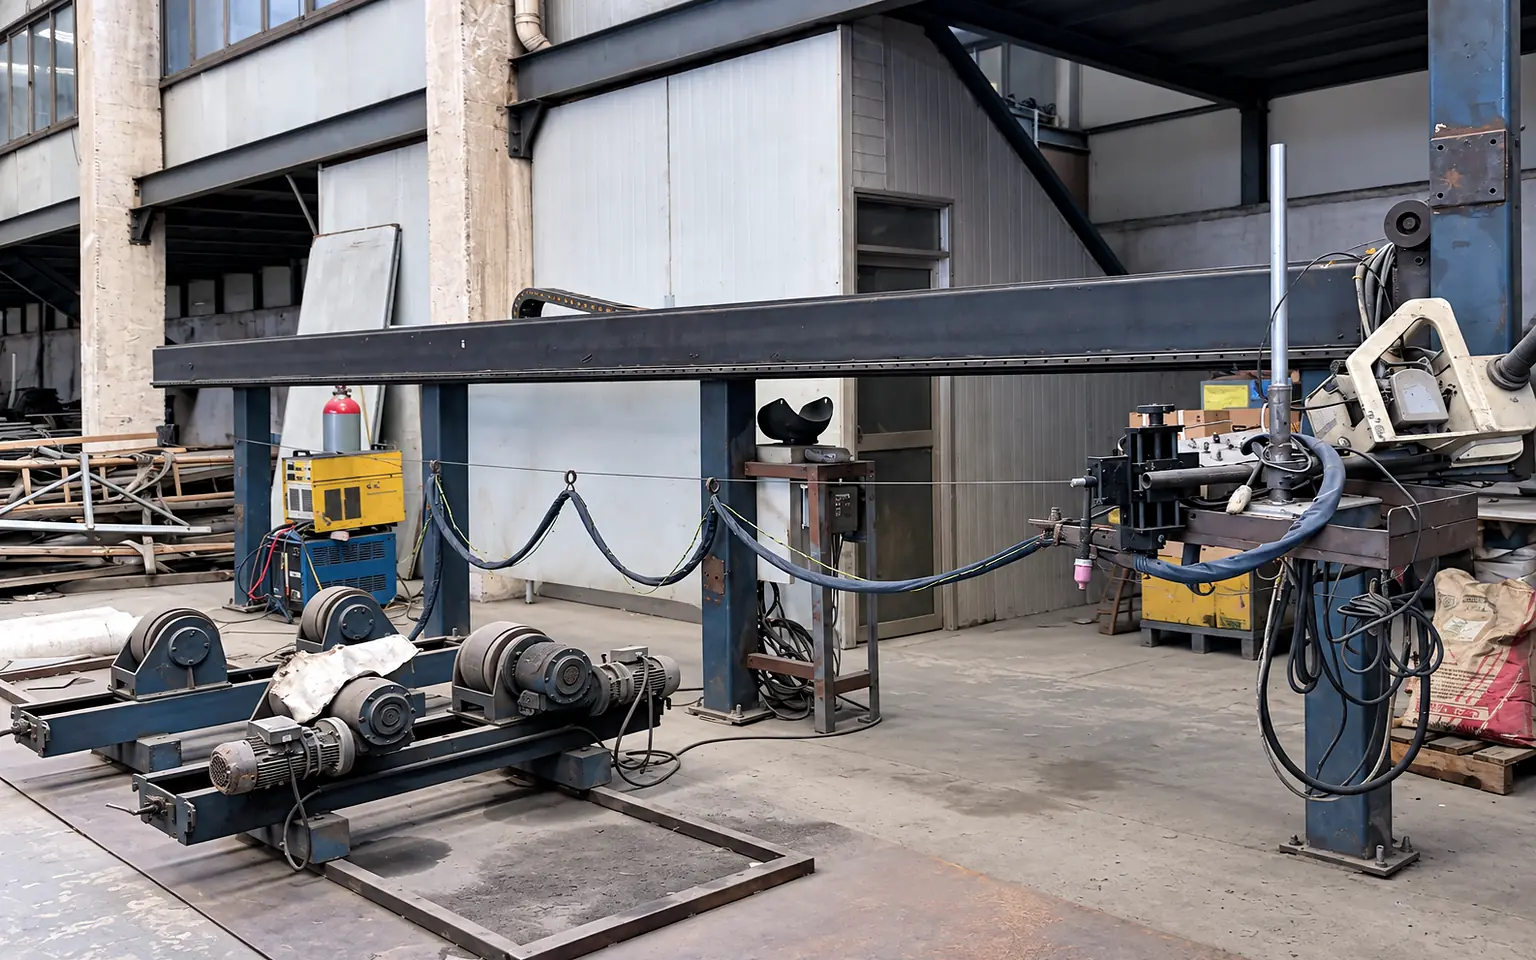 04
Manual TIG Welding
GTAW · LOCAL CONTROL & REPAIRManual torch and filler control suit complex positions, short transitions, localized filling and qualified repair work. It is also used where mechanized access is limited.
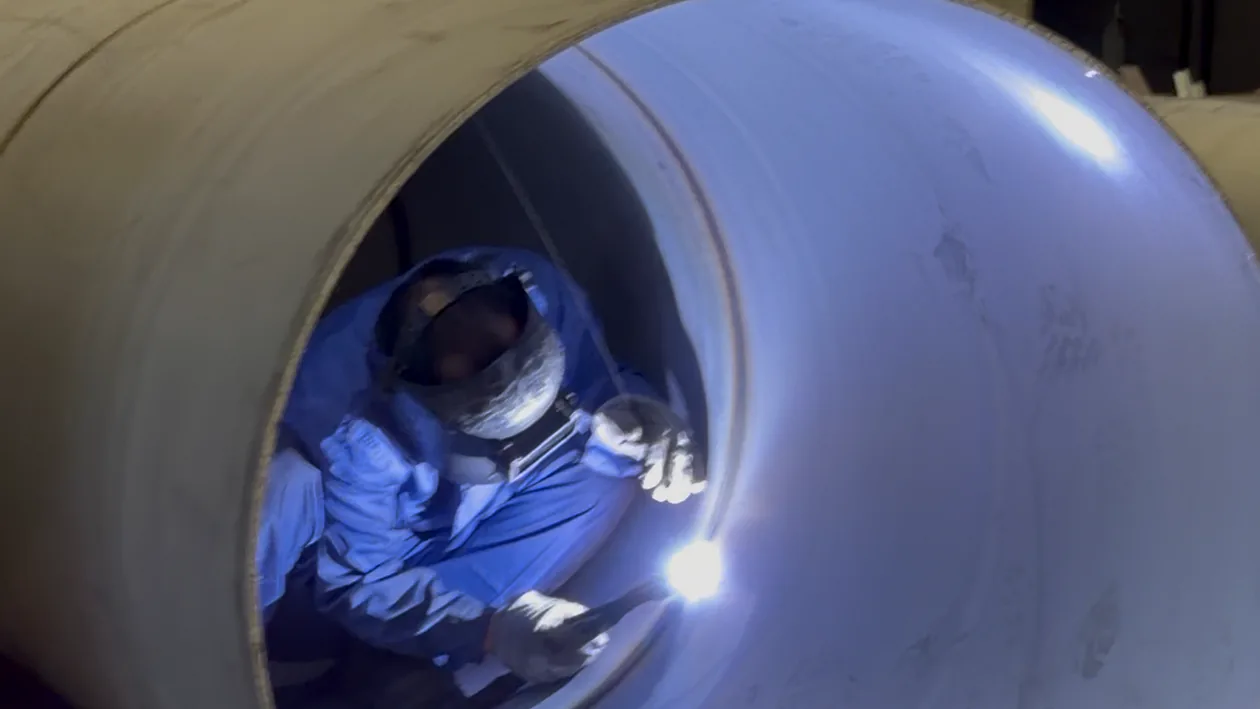 05
Shielded Metal Arc Welding
SMAW · MANUAL ARC WELDINGCovered electrodes support suitable positional fabrication and localized maintenance or repair. Electrode classification, storage, preparation and interpass cleaning are controlled by the approved route.
10 MM JOINT EXAMPLE
Welding Route Combinations
Choose a route to see how one stainless steel joint may divide the root and remaining fill/cap between compatible processes.
PAW Root + Mechanized GTAW Fill/Cap
A concentrated plasma root establishes penetration and back formation. Mechanized GTAW then completes the remaining fill and cap with controlled travel and shielding.
- Suitable where bead consistency and surface control are priorities.
- Internal formation is checked before additional conditioning.
- NDT and acceptance follow the project requirement.
PAW Root + SAW Fill/Cap
After the plasma root, submerged arc welding supplies efficient fill and cap deposition on a suitable longitudinal joint using the specified wire and flux system.
- Process selection considers joint position, seam length and access.
- Flux handling and interpass cleaning are part of route control.
- Heat input remains governed by the applicable procedure.
PAW Root + Manual GTAW Fill/Cap
The plasma root is followed by manual GTAW where local access, joint transitions or controlled filler placement favor direct operator control.
- Useful for shorter seams and complex geometry.
- Also supports localized qualified repair after examination.
- Pass sequence and cleaning remain procedure-controlled.
Illustrative 10 mm joint example. Final groove geometry, pass sequence and welding parameters follow the applicable pWPS/WPS and approved project requirements.
INTERNAL WELD CONDITIONING
Control Continues Behind the Root
Root completion is not the end of the joint review. Internal bead shape, continuity and project acceptance requirements determine whether further internal conditioning is needed.
Review root formation, reinforcement, continuity and accessible surface condition.
Determine whether dressing, GTAW fusion conditioning or an internal SAW pass is applicable.
Apply the approved internal operation with defined access, cleanliness and interpass controls.
Re-examine the internal seam against the order-specific visual and inspection criteria.
PWPS / WPS LOGIC
Welding Procedure Control
These public summaries explain the route logic without exposing controlled procedure documents or proprietary production parameters.
316L · PAW + SAW
- Base material
- EN 10088-2 · 1.4404 / 316L · material group 8.1.
- Joint / record thickness
- Plate butt joint in PA position · representative record at 24 mm.
- Sequence
- PAW root followed by SAW fill and cap passes.
- Filler approach
- ER316L deposition with the specified wire and flux system.
- Control focus
- Root shielding, flux handling, layer cleaning and interpass control.
- Inspection route
- Visual, dimensional and order-agreed NDT stages.
- Standard / status
- EN ISO 15614-1:2004 + A2:2012 · NOKX-controlled pWPS summary.
2205 · PAW + GTAW
- Base material
- EN 10088-2 · 1.4462 / 2205 · material group 10.1.
- Joint / record thickness
- Plate butt joint in PA position · representative record at 10 mm.
- Sequence
- PAW root with mechanized GTAW outer and internal conditioning passes.
- Filler approach
- Representative route uses GTAW fusion passes without separate filler addition.
- Control focus
- Internal seam formation, shielding and route-specific interpass control.
- Inspection route
- Visual, dimensional and order-agreed NDT stages.
- Standard / status
- EN ISO 15614-1:2004 + A2:2012 · NOKX-controlled pWPS summary.
316L / 2205 · Manual GTAW
- Base materials
- 1.4404 / 316L group 8.1 and 1.4462 / 2205 group 10.1.
- Joint / record thickness
- Plate butt joint in PA position · representative records at 6 mm and 20 mm.
- Sequence
- Manual GTAW root, fill and cap for controlled local access.
- Filler approach
- ER316L or ER2209 selected to match the base material route.
- Control focus
- Joint preparation, filler placement, cleaning and interpass control.
- Inspection route
- Visual, dimensional and order-agreed NDT stages.
- Standard / status
- EN ISO 15614-1:2004 + A2:2012 · NOKX-controlled pWPS summary.
STANDARDS FRAMEWORK
Qualification and Product Requirements
Procedure qualification rules and product specifications play different roles. NOKX reviews both against the customer drawing, specified edition and order acceptance requirements.
How the Welding Route Is Qualified
- ASME BPVC Section IX · welding procedure and personnel qualification framework.
- ISO 15614-1 / EN ISO 15614-1 · procedure test framework for arc and gas welding of steels and specified alloys.
What the Manufactured Product Must Meet
- ASTM A312/A312M · stainless steel pipe product specification.
- ASTM A358/A358M · electric-fusion-welded austenitic stainless steel pipe specification.
The exact edition is recorded from the applicable project document and qualified welding procedure. Existing qualifications are identified by their real edition; website text does not silently substitute a newer year.
INSPECTION, REPAIR & RECORDS
Control at Every Welding Stage
Inspection points are coordinated with the order and applicable acceptance criteria. Specific NDT methods and documentation are confirmed during technical review.
Groove, cleanliness and edge condition.
Fit-up, mismatch and access review.
Penetration and back formation control.
Cleaning, sequence and temperature limits.
Bead placement and surface profile.
Order-specified method and acceptance.
Remove the indication to sound metal, then repair.
Recheck the repaired area and close records.
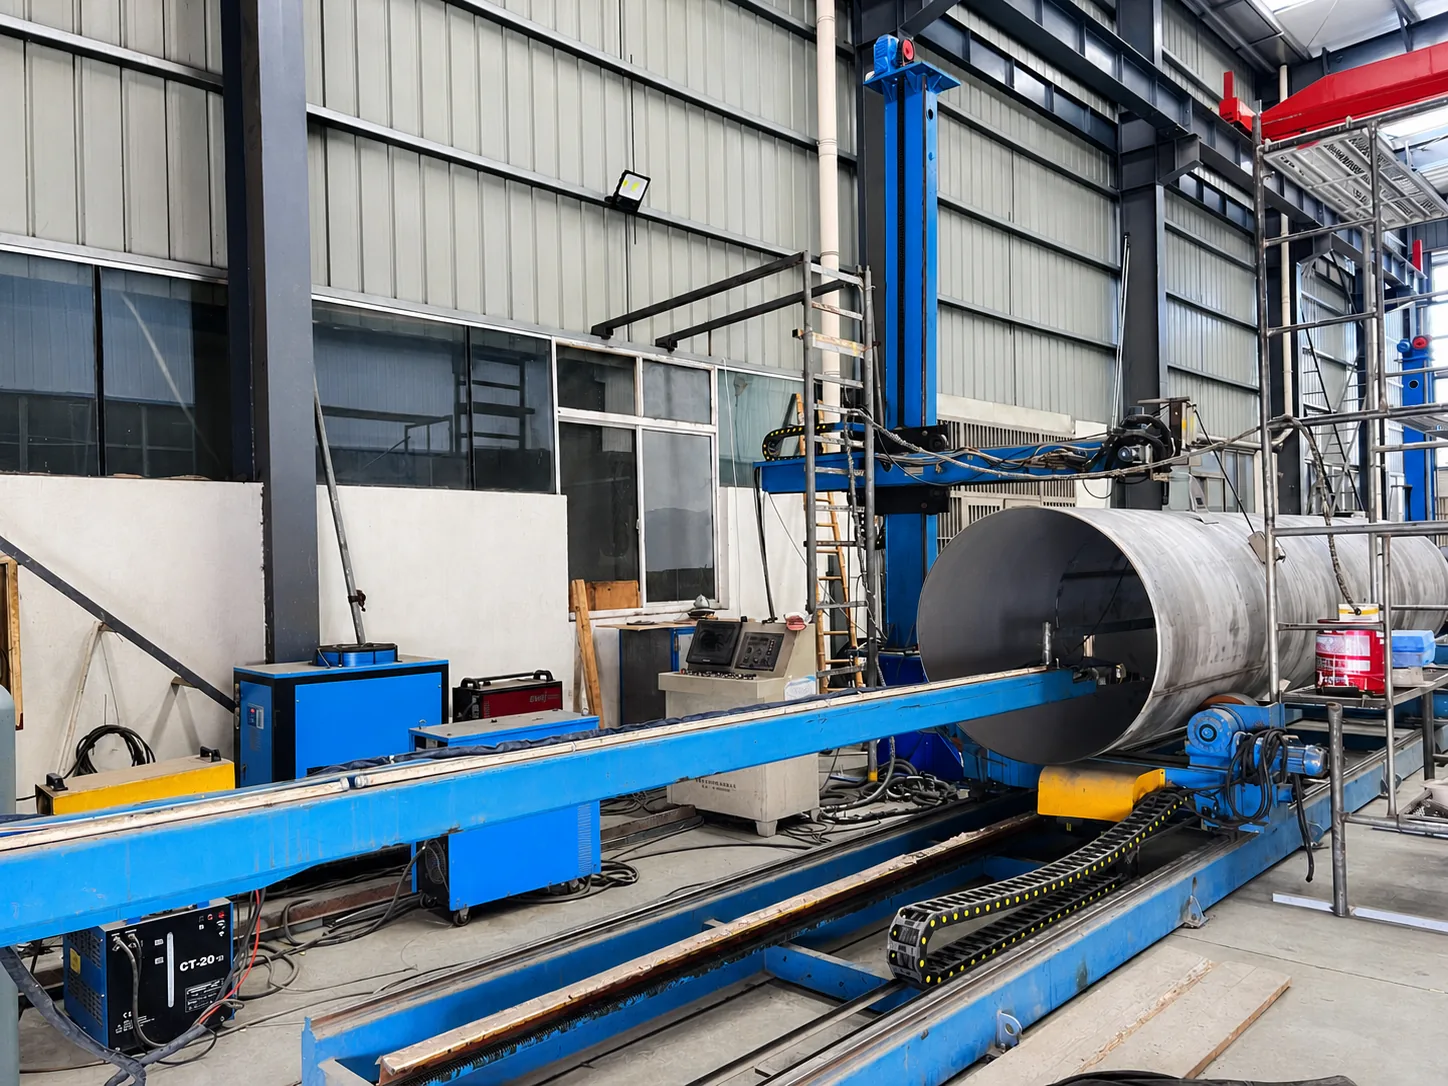
EQUIPMENT & WORKSHOP EVIDENCE
See the Process Environment
RELATED PRODUCTS
Products Supported by Welding Control
Review the current NOKX product range. Individual product pages will become the destination as they are published.
WELDING FAQ
Questions Before Technical Review
Which welding process is suitable for my product?
The choice depends on material, thickness, joint geometry, welding position, seam length, access, product standard and inspection requirement. NOKX reviews these inputs before confirming a route.
Can several welding processes be combined in one joint?
Yes. A qualified route may assign the root, fill, cap, internal conditioning and repair to different compatible processes. The combination must follow the applicable procedure and project approval.
Can plasma welding achieve single-side welding with back formation?
For suitable stainless steel joints at 10 mm and below, plasma root welding may achieve single-side welding with back formation under a qualified procedure. Joint design and material condition still require review.
How are internal weld beads treated?
The internal root profile is inspected first. Where the joint requires additional conditioning, a GTAW fusion pass without separate filler addition or an internal SAW pass with the specified wire and flux system may be considered.
Which standards can be followed?
Procedure qualification may reference ASME BPVC Section IX or ISO/EN ISO 15614-1, while the product may be ordered to specifications such as ASTM A312/A312M or ASTM A358/A358M. The exact standard and edition must be confirmed for the project.
How are weld defects repaired?
The indication is evaluated and removed to sound metal. A qualified manual GTAW or other applicable repair process is then used, followed by re-examination to the agreed acceptance criteria.
What inspection documents can be supplied?
Welding and inspection records are supplied when applicable to the product, order and agreed inspection requirements. Available document types are confirmed during quotation and technical review.
What information should I send for a welding review?
Send the product drawing, joint location, material grade, nominal thickness, required standard and edition, quantity, inspection method, acceptance criteria and any project-specific documentation requirements.
PROJECT-SPECIFIC REVIEW
Send the Joint, Material and Acceptance Requirements
Provide your drawing, material grade, thickness, applicable standard and inspection needs for route review and quotation.